

Process approach
How is this process handled?
01 · InputMaterial + geometry
02 · ProcessLocalized surface hardnessControlled depth
03 · VerificationMeasurement + reporting
Technical explanation
Working principle
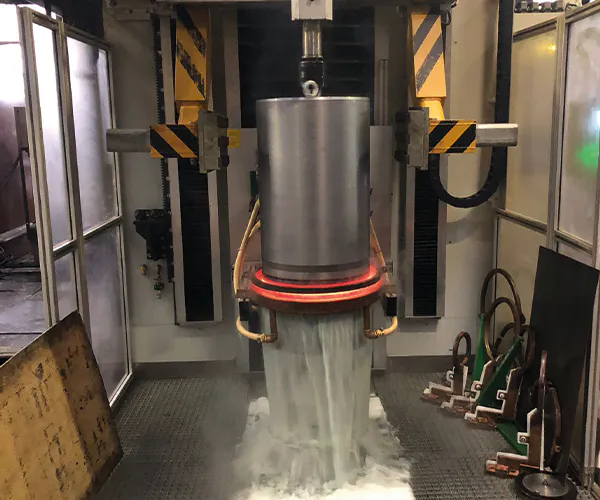
An alternating electromagnetic field induces eddy currents in the workpiece and heats the selected surface zone. Immediate quenching transforms this zone into a hard, wear-resistant layer.
Process selection
Low frequency is preferred for larger parts and deeper layers; high frequency supports smaller parts and shallower layers. Coil geometry, distance, power, rotation and quenching are engineered for uniform results.
Benefits
- Localized treatment and short heating times
- Low oxidation and limited distortion
- Improved fatigue and wear resistance
- Integration into serial production lines